Mark presence
Confirm that the complete laser-marked field exists in the expected product area.
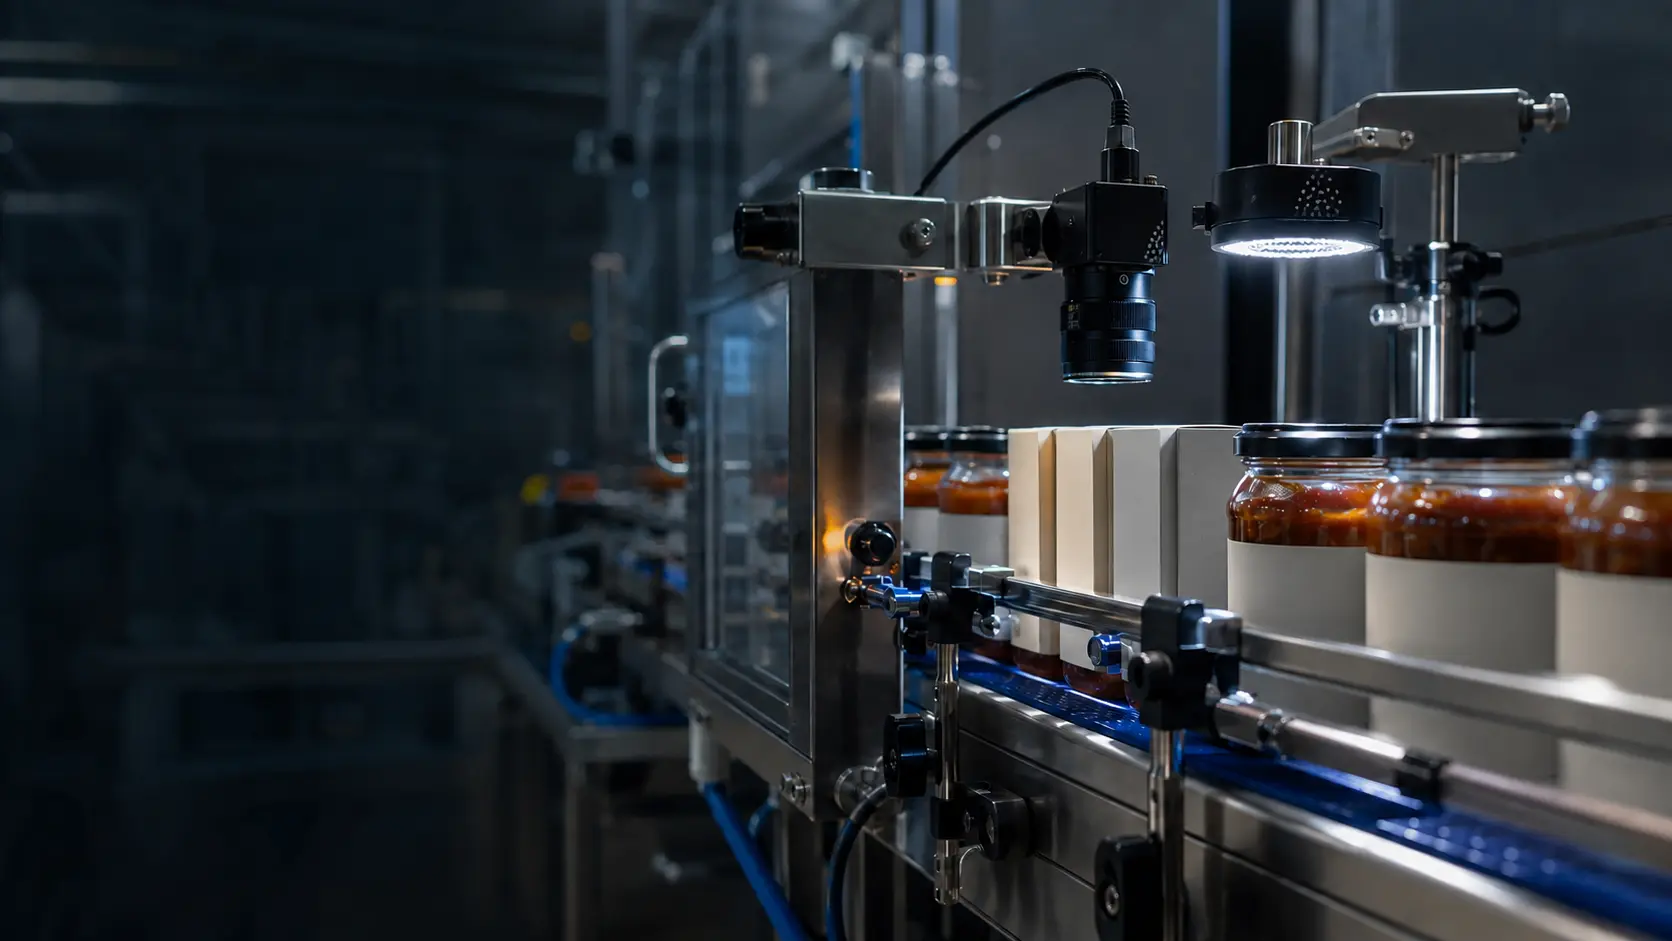
Use controlled illumination and machine vision to inspect low-contrast laser dates, batch details and lot codes across reflective, curved and textured surfaces.
Laser marking changes the substrate rather than applying ink. Contrast can therefore depend heavily on material, colour, surface finish and viewing angle. Oxford Vision Systems trials optical arrangements that reveal the mark consistently without being distracted by pack texture or reflections.
Confirm that the complete laser-marked field exists in the expected product area.
Read or compare dates, batches and lot strings using OCR or OCV tools.
Distinguish shallow, pale or surface-dependent marks from the surrounding material.
Detect a displaced code that falls outside the approved marked zone.
A sample-led optical trial determines whether the code can be captured reliably across the real material, product position and permitted production variation.
Use lighting geometry, exposure and polarisation to reduce glare from glossy surfaces.
Confirm the permanent mark contains the date or traceability string required for the job.
Identify faint, incomplete or misplaced laser codes before downstream packing.
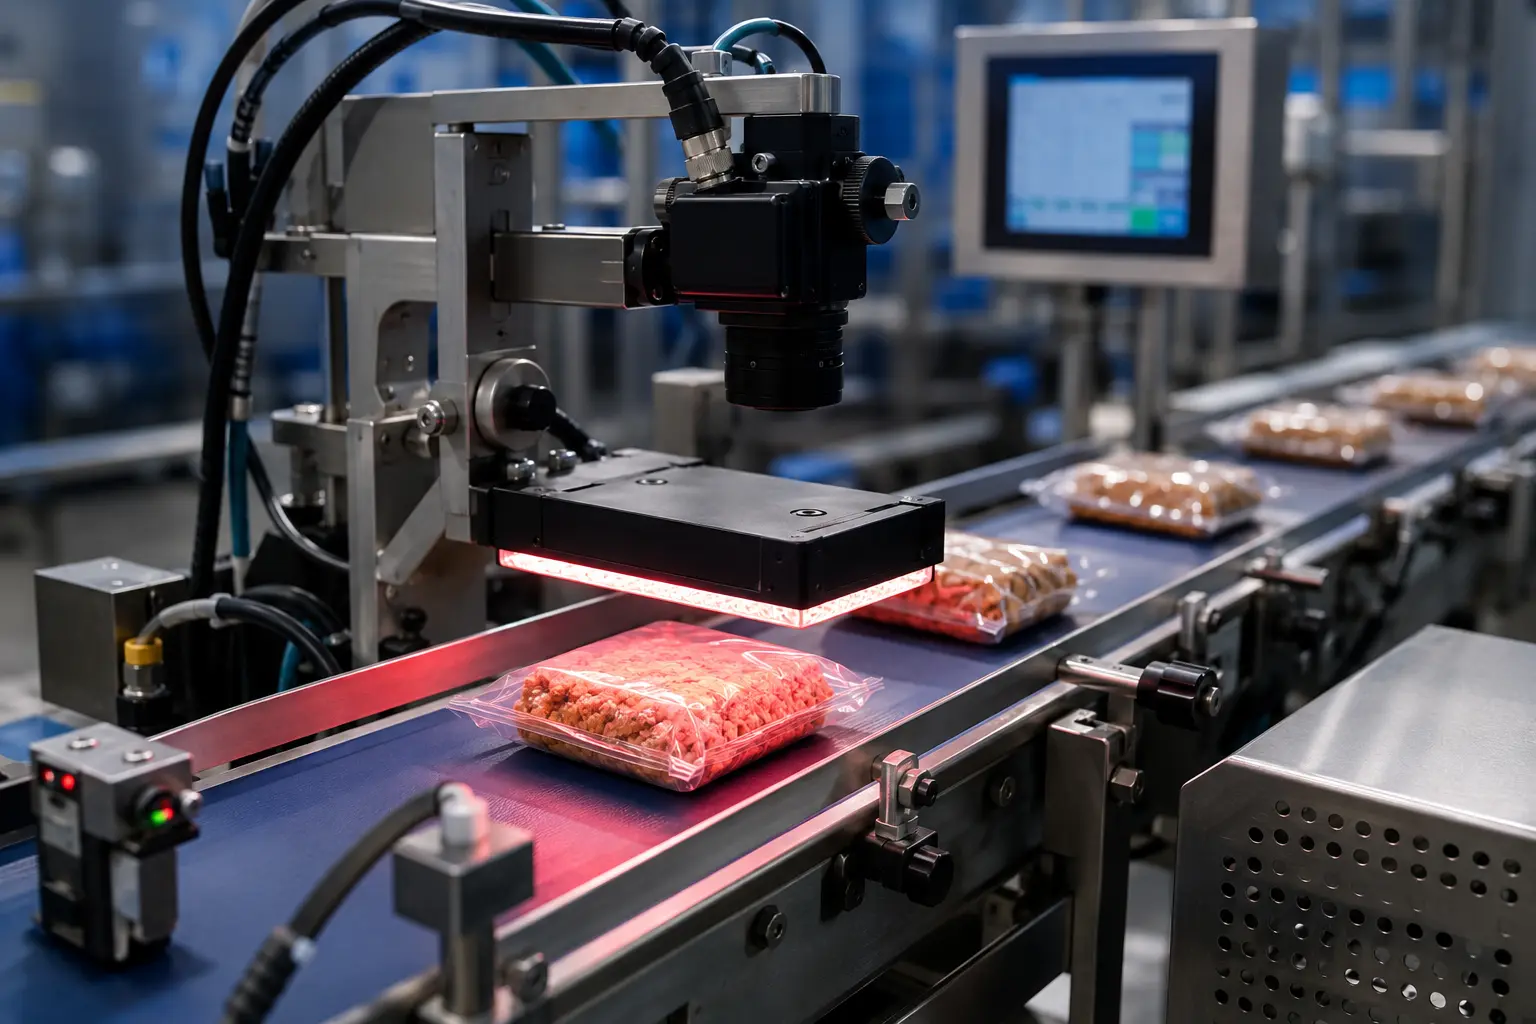
A successful setup must work across approved material batches, moulding variation and product orientation. We assess the weakest legitimate mark as well as known defects before fixing the inspection threshold.
Combine the inspection with complementary print, data or reject checks where they reduce the risk of a non-conforming pack reaching the customer.
Every inspection begins with real samples, representative print and the operating conditions found on your production line.
Often, but the result depends on the material and the physical change created by the laser. Trials may use directional, diffuse, dark-field or polarised lighting to reveal the mark.
Potentially, yes. Bottle curvature, transparency, contents, surface reflections and rotational position all influence the optical design and must be represented in the trial.
A vision system can measure visible characteristics such as contrast, completeness and character shape. It does not directly measure laser power, but it can identify the resulting mark degradation.
Provide representative materials, the lightest acceptable mark and known failures. We will evaluate the optical approach before integration.