Product tracking
Maintain pack identity between the inspection trigger and downstream reject position.
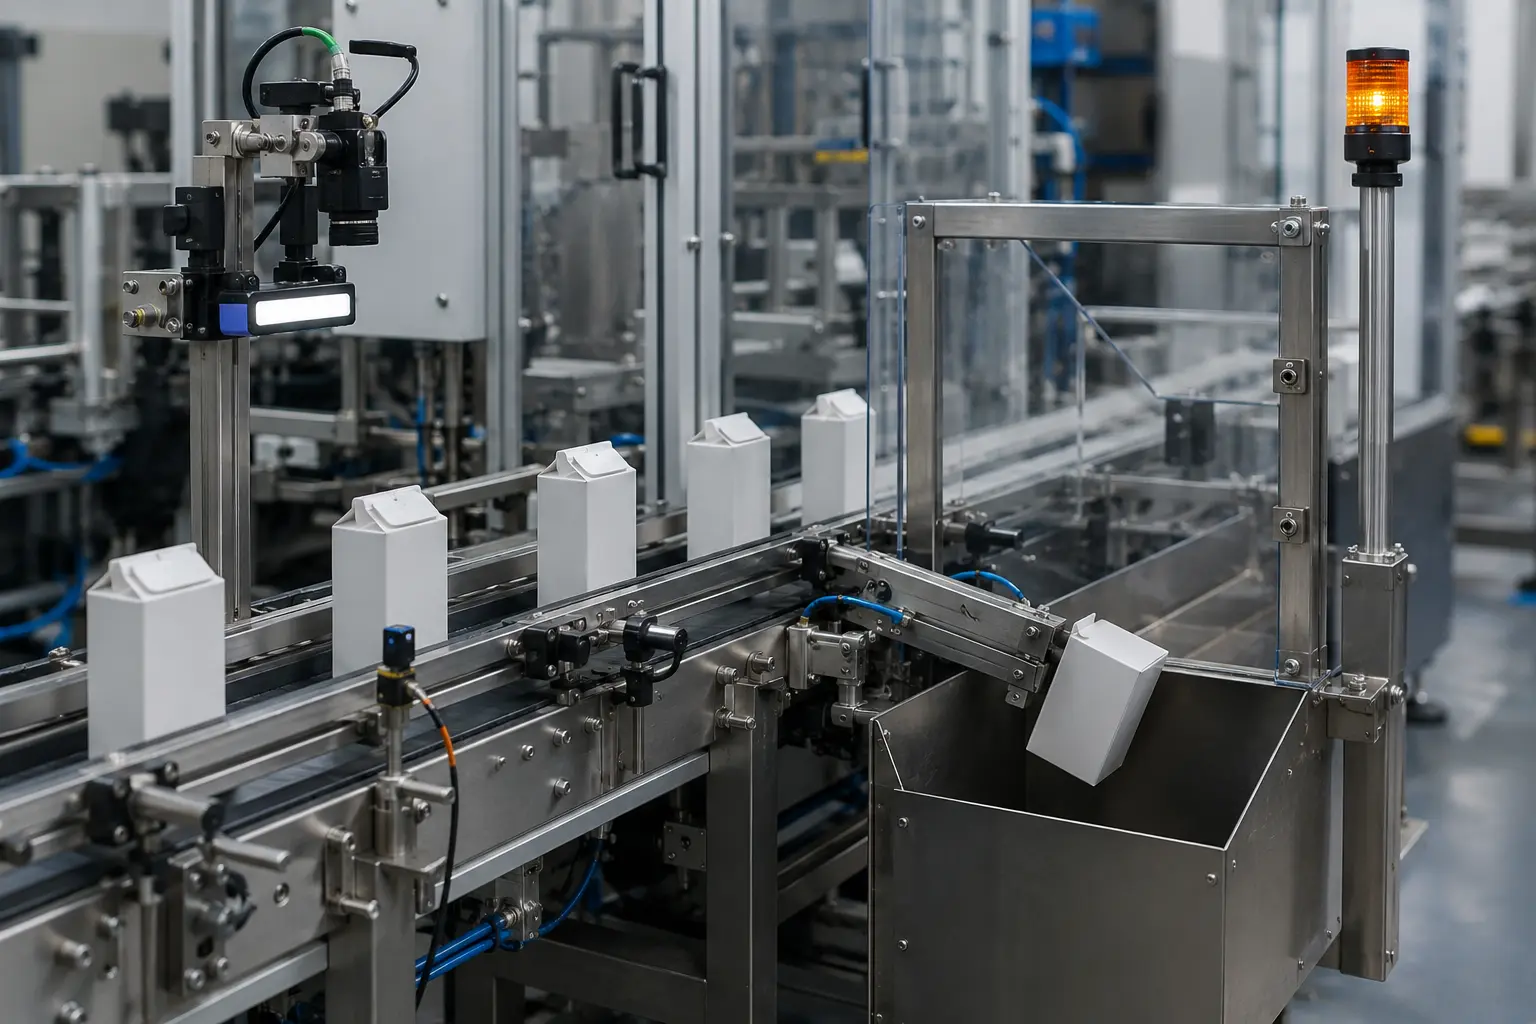
Track the inspected product from camera to reject point, activate the correct device and confirm that the non-conforming pack has left production.
Oxford Vision Systems integrates reject hardware, sensors and line logic around the product format and risk. The system can identify an individual failed pack, track its movement and verify removal into a secure collection area.
Maintain pack identity between the inspection trigger and downstream reject position.
Select air blast, pusher, drop flap, diverter or line stop according to pack behaviour.
Use sensors to prove the failed product reached the reject path or container.
Monitor full bins, air pressure, access doors, sensor health and consecutive failures where required.
A complete solution manages the failure from image decision through physical segregation, with clear states for operators and line controls.
Remove individual failures without unnecessarily stopping normal production where the application permits.
Detect a successful reject and trigger a controlled fault if the expected confirmation is absent.
Use lockable bins and monitored access for applications that require controlled segregation.
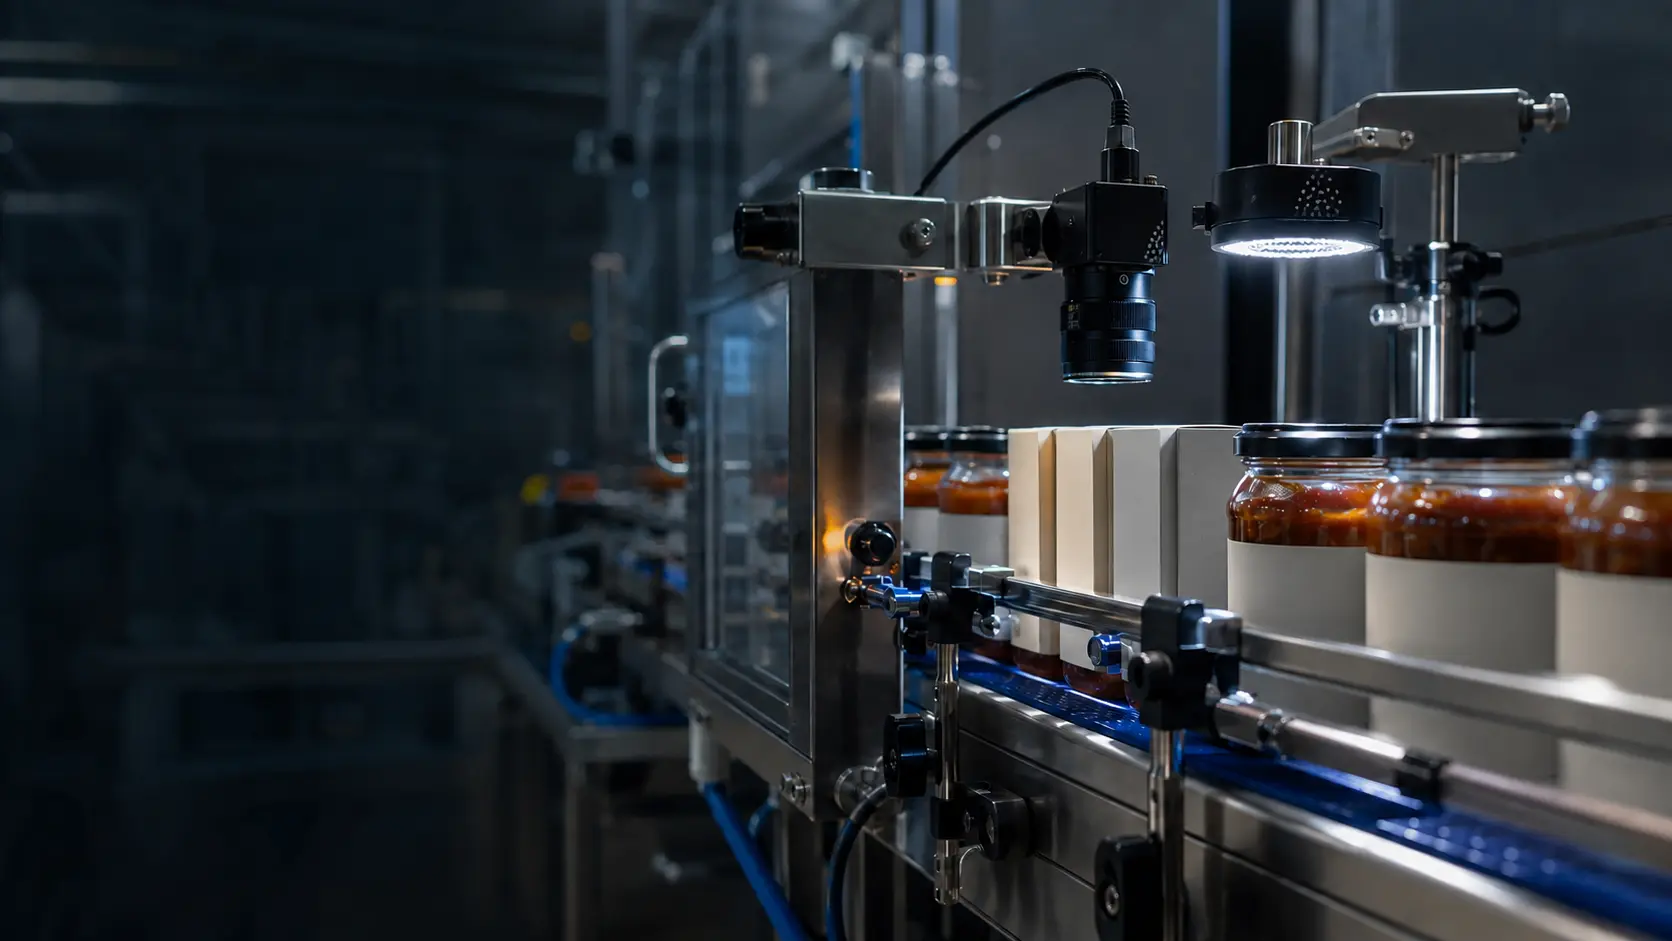
A light pouch may suit air rejection, while a heavy container may need a positive pusher or conveyor diversion. We consider centre of gravity, conveyor speed, product spacing, available distance, guarding and what happens when utilities fail.
Combine the inspection with complementary print, data or reject checks where they reduce the risk of a non-conforming pack reaching the customer.
Every inspection begins with real samples, representative print and the operating conditions found on your production line.
It depends on the pack. Air jets suit some light products; pneumatic pushers, drop flaps and powered diverters suit others. The choice is proven using actual products at representative speed.
The controls track the failed product from its camera trigger using encoder or sensor events and activate the reject when that product reaches the reject point.
Yes. A downstream sensor can verify that the failed product entered the reject route. Missing confirmation can initiate an alarm and line stop according to the agreed control philosophy.
Share your pack format, conveyor layout, speed and risk requirements. We will recommend a reject method and confirmation sequence.